Indpro Logo

Indpro
Typically replies within an hour

Indpro
"Hello!👋

How can I help you today with your bulk material handling needs?"
×
Chat with Us

Why Pneumatic Conveying Lines Get Blocked & How to Prevent It
Why Pneumatic Conveying Lines Get Blocked & How to Prevent It

Pneumatic conveying is widely used to transport powders, granules, pellets and bulk solids because it offers flexible routing, enclosed material handling, and high levels of automation. But when conveying conditions move outside their stable operating range, one problem can bring the entire process to a halt: ‘pipeline blockage’.

A blockage is rarely caused by the pipe alone. In most cases, it is the result of an imbalance between air velocity, solids loading, pressure drop, material properties, and pipeline geometry.

Understanding the engineering principles behind these variables is the key to preventing recurring blockages.


What Actually Causes a Pneumatic Conveying Line to Block?

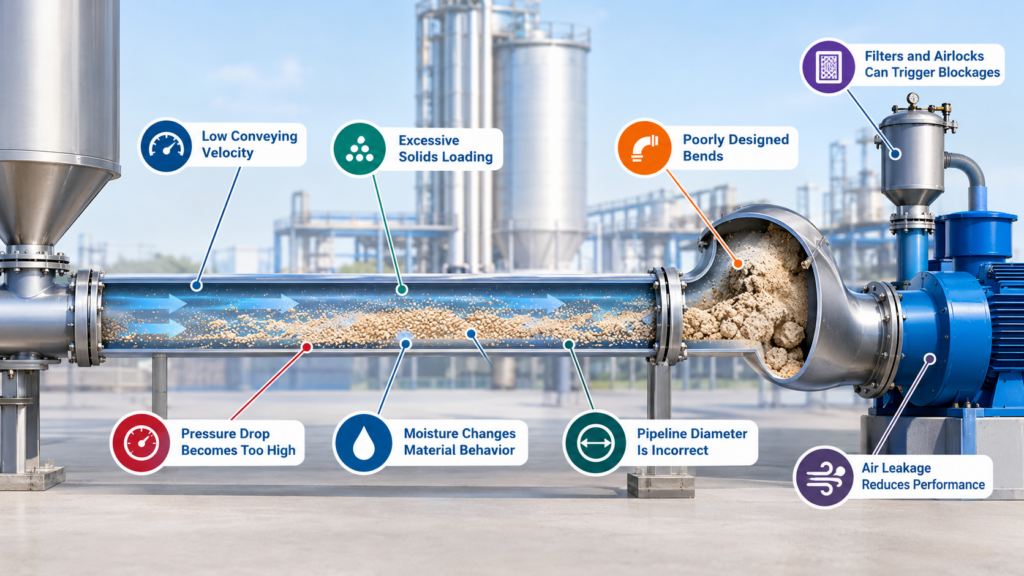
Pneumatic Pipeline Blockage Infographic

For material to move reliably, the conveying air must generate sufficient drag to transport the particles through the pipeline. If the available conveying force becomes insufficient, particles begin to settle.

This is particularly important in horizontal sections, bends, reducers, and other areas where pressure losses are higher.

The process can become self-reinforcing:

Lower airflow → particle settling → increased resistance → higher pressure drop → further reduction in conveying performance → blockage.

Therefore, the objective should not simply be to clear a plugged line. The real engineering objective is to identify what caused the system to leave its stable conveying envelope.

 1. Low Conveying Velocity

One of the most common causes of blockage is insufficient air velocity.

Every material has a range of conveying conditions below which particles can begin to settle. In dilute-phase conveying, this is commonly discussed in terms of saltation velocity – the approximate condition at which particles begin to deposit rather than remain effectively transported.

The required velocity depends on:

  • Particle size and density
  • Particle shape
  • Bulk density
  • Moisture
  • Cohesiveness
  • Solids loading
  • Pipeline diameter
  • Conveying pressure
A blower can be running normally while the actual velocity inside the pipeline is too low.
 
Engineering principle: Continuity

For a given gas stream, the relationship between flow rate and velocity is expressed by:
Q = A x V
 
where:
  • Q = volumetric airflow
  • A = pipeline cross-sectional area
  • V = average air velocity
This means that increasing pipeline diameter without increasing airflow reduces velocity.
 
Prevention: Establish a minimum stable conveying velocity for the specific material and verify actual airflow rather than assuming that blower operation equals adequate conveying.
 

 2. Excessive Solids Loading

 The opposite problem can also cause a blockage.

If too much material is introduced into the pipeline without sufficient conveying air, the solids-to-air ratio increases. The air stream may no longer have enough momentum and drag to maintain stable transport.

This can happen when:

  • Feed rate is increased
  • A rotary airlock is oversized
  • Material bulk density changes
  • A feeder operates above its design rate
  • Material enters the line in slugs
The result can be rapid material accumulation.

A system designed for a particular solids loading should therefore not be operated continuously beyond that envelope simply to increase production.

A stable 8 tonnes/hour can be more productive over a year than an unstable 10 tonnes/hour system that repeatedly blocks.

 3. Pressure Drop Becomes Too High

 Every pneumatic conveying system experience pressure loss due to friction, fittings, bends, valves, acceleration of solids, and elevation changes.

For gas flow through a straight pipe, a useful engineering relationship is the Darcy-Weisbach equation:


where:

  • ΔP = pressure loss
  • f = friction factor
  • L = pipe length
  • D = pipe diameter
  • ρ = gas density
  • V = gas velocity
Although pneumatic conveying calculations must additionally account for solids, the equation illustrates an important principle: pipeline geometry, velocity, density, and length directly influence pressure loss. 
 
A long pipeline with numerous bends and restrictions can therefore require substantially more pressure than a simple straight line.
 
Prevention: Calculate the complete system pressure balance, including straight pipe, fittings, bends, elevation, filters, valves, and material acceleration.
 

 4. Poorly Designed Bends

 Bends are most prominent locations for material accumulation.

When particles change direction, their inertia causes them to resist the change in motion. Larger or denser particles can impact the outer wall of the bend, while cohesive or fragile materials may accumulate or degrade.

Poor bend design can therefore produce:

  • Material deposition
  • Erosion
  • Product degradation
  • Excessive pressure loss
  • Repeated plugging 
The number, radius, and orientation of bends should be considered during system design rather than treated as simple pipe-routing decisions. 
 
Engineering principle: Minimize unnecessary fittings and select bend geometry according to the material’s conveying characteristics.
 

 5. Moisture Changes Material Behavior

 Moisture is particularly problematic for powders.

A material that flows freely when dry can become cohesive when exposed to humidity. Fine particles may agglomerate, stick to the pipe wall, or form deposits.

Moisture can alter:

  • Bulk density
  • Cohesiveness
  • Flowability
  • Particle size
  • Angle of repose 

Therefore, the conveying system may effectively be handling a different material from the one used during its original design.

Prevention: Control material moisture, prevent condensation, maintain appropriate conveying-air conditions, and keep moisture-sensitive materials properly sealed. 

 6. Pipeline Diameter Is Incorrect

 Pipeline diameter must be selected together with airflow, pressure, and material characteristics.

An undersized pipe can produce excessive pressure drop and high particle velocity. An oversized pipe can reduce velocity below the stable conveying range if airflow is not increased.

This is another application of the continuity relationship:

V = Q / A

Increasing diameter increases area, so the same airflow produces a lower velocity.

The largest possible pipe is therefore not necessarily the best pipe.

Good design balances velocity, pressure drop, energy consumption, wear, and material handling requirements. 

 7. Air Leakage Reduces Conveying Performance

 Pneumatic conveying depends on controlled airflow. Leaks around flanges, gaskets, valves, inspection covers, and flexible connections can reduce the air actually available for material transport.

The result may be:

Designed airflow ≠ Actual conveying airflow

This is especially important in systems operating close to their minimum conveying conditions.

Routine inspection of joints and flexible connections, combined with airflow and pressure monitoring, can identify developing problems before they become blockages.

 8. Filters and Airlocks Can Trigger Blockages

 A conveying line does not operate independently of its connected equipment.

A dirty filter increases resistance. A worn rotary airlock can allow excessive air leakage. A malfunctioning feeder can introduce material inconsistently.

These failures can change the system’s pressure and airflow balance.

Pressure-drop monitoring is therefore valuable.

A gradual increase in differential pressure across a filter may indicate fouling. An unexpected change in conveying-line pressure may indicate restriction, leakage, or altered material loading.

This turns instrumentation into an early-warning system rather than simply a method of displaying operating conditions.
How to Prevent Pneumatic Conveying Blockages

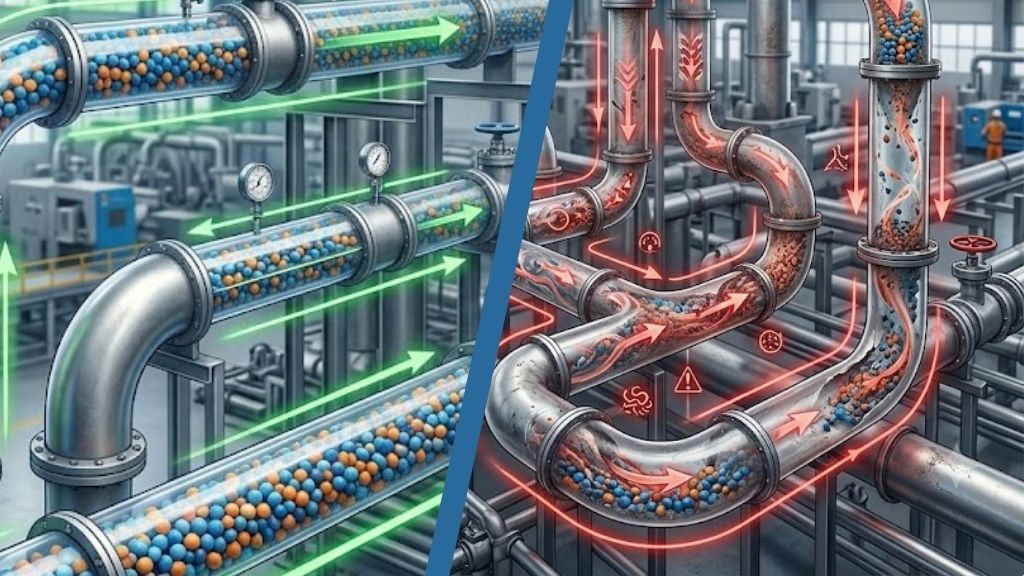
 1. Operate Above the Minimum Stable Conveying Velocity

Determine the appropriate operating window through material testing, system calculations, and commissioning data.
 
Do not simply choose an arbitrary velocity.
 
The optimum velocity should be high enough to prevent settling but not unnecessarily high, because excessive velocity can increase energy consumption, erosion, and product degradation.
 

 2. Control Solids Loading 

Maintain a stable relationship between material feed rate and conveying airflow.

Avoid sudden increases in feeder speed unless the conveying system has sufficient capacity to handle the additional solids.

Stable feeding is particularly important in dense-phase applications.

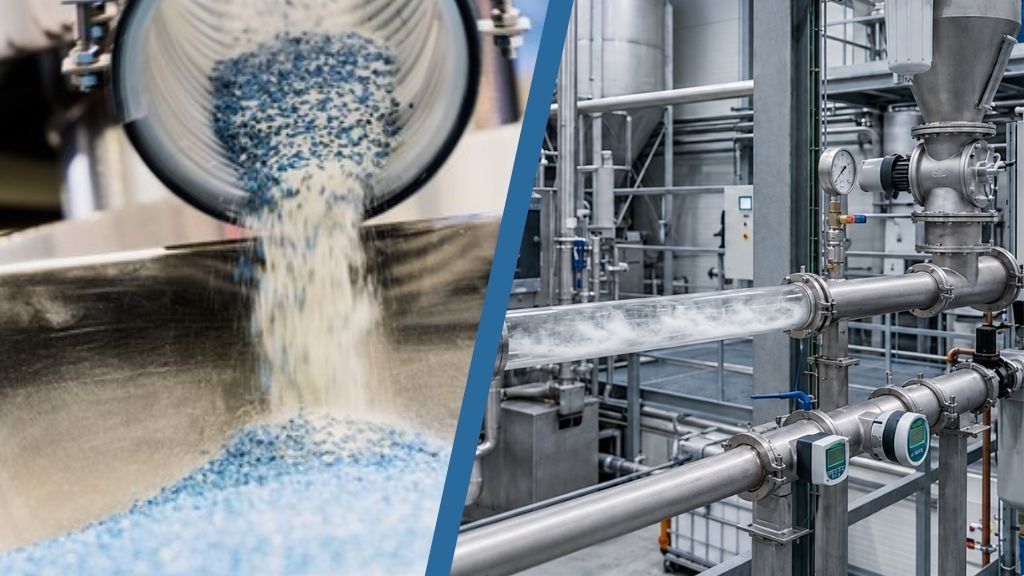
 3. Monitor Pressure and Airflow 

A modern pneumatic conveying system should ideally monitor:
  • Blower discharge pressure
  • Pipeline pressure
  • Differential pressure across various conveying elements
  • Airflow
  • Filter differential pressure
  • Material feed rate

Trend data are often more useful than individual readings. 

For example:
 
Normal pressure trend → Stable operation
 
Gradually increasing pressure → Possible accumulation
 
Rapid pressure increase → Potential developing blockage
 
The exact alarm limits should be established for the specific installation.
 

 4. Account for Material Variability

Do not design or operate a conveying system based solely on nominal material properties.
 
Monitor changes in:
 
  • Moisture
  • Particle-size distribution
  • Bulk density
  • Temperature
  • Cohesiveness
  • Product formulation
Material testing is therefore an important part of both new system design and troubleshooting.


Reactive Troubleshooting vs. Predictive Engineering


A common plant response to blockage is:

Stop → Clear pipe → Restart → Continue production.

That solves the immediate symptom but not the engineering problem.

A better approach is:

Detect → Analyze → Correct → Monitor.

If a line repeatedly blocks at the same location, investigate:

1. Where does accumulation begin?

2. What was the airflow at that moment?

3. What was the pipeline pressure?

4. What was the solids feed rate?

5. Had the material properties changed?

6. Was there a filter, valve, feeder, or airlock problem?

Repeated blockage at the same location is valuable diagnostic information. It usually indicates a recurring local condition rather than random failure.


A Practical Blockage-Prevention Checklist


✅ Verify minimum conveying velocity

✅ Maintain stable solids loading

✅ Calculate total system pressure drop

✅ Minimize unnecessary bends and restrictions

✅ Select pipeline diameter based on actual operating conditions

✅ Control material moisture

✅ Check for air leakage

✅ Inspect filters and airlocks


Final Takeaway


Pneumatic conveying blockages are usually a system-balance problem, not simply a pipe problem.

The most reliable systems maintain the correct relationship between air velocity, solids loading, pressure drop, material properties, and pipeline geometry.

Engineering principles such as the continuity equation and Darcy-Weisbach pressure-loss relationship provide the foundation for understanding these relationships. But successful pneumatic conveying also requires attention to real-world factors such as moisture, particle behavior, feeder stability, bends, filters, and changing raw-material characteristics.

The goal should not be to design a system that merely conveys material at maximum capacity. The goal is to design one that conveys consistently, efficiently, and predictably within a stable operating window.

That is the difference between a pneumatic conveying system that simply works – and one that delivers reliable plant performance year after year. This is where Indpro makes a difference.