
Designing Pneumatic Conveying Systems for Fragile Materials
Designing Pneumatic Conveying Systems for Fragile Materials
Pneumatic conveying is widely used across industries to transport bulk solids through enclosed pipelines using air or gas as the conveying medium. Its flexibility, clean operation, reduced material handling, and ease of automation make it an attractive solution for modern manufacturing facilities. However, when the material being transported is fragile, system design becomes significantly more complex.
Unlike robust bulk solids, fragile materials can fracture, chip, abrade, or generate excessive fines when exposed to high velocities, sudden acceleration, particle-to-particle collisions, and repeated impacts against pipeline walls. These changes can compromise product quality, reduce yield, increase waste, and affect downstream processing performance.
Fragile materials are found across several industries, including food processing, polymers, chemicals, petrochemicals, and minerals. Examples include breakfast cereals, spray-dried food powders, roasted coffee beans, expanded polymer beads, polymer pellets, pharmaceutical granules, chemical catalysts, and porous mineral granules. Although these materials differ in composition and application, they share a common engineering requirement: they must be conveyed without unacceptable degradation.
The challenge is therefore not simply to move material efficiently, but to balance product integrity, conveying reliability, energy consumption, and overall operating cost. Achieving this balance requires a material-specific approach to pneumatic conveying system design.
Understanding Fragility Across Different Industries
The first step in designing a pneumatic conveying system is understanding how the material responds to mechanical stress. Fragility is not determined by particle size or bulk density alone. It depends on particle structure, fracture strength, shape, moisture content, surface characteristics, and sensitivity to impact and abrasion.
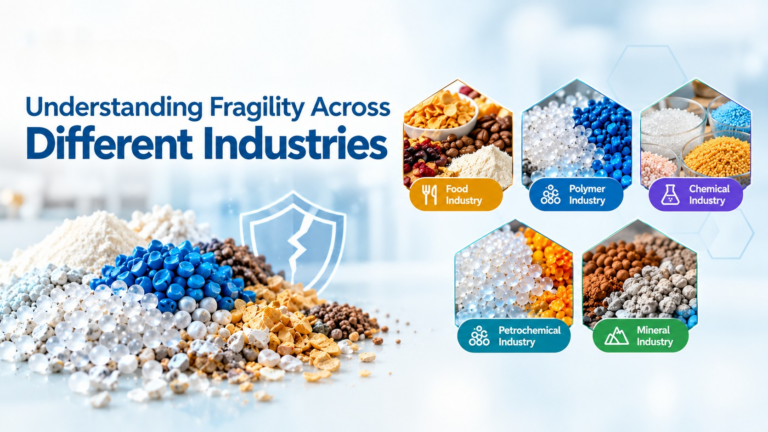
Different industries illustrate these challenges particularly well.
- Food industry: Breakfast cereal pieces, puffed rice, extruded snacks, dried fruit pieces, roasted coffee beans, spray-dried milk powder, and delicate food granules can experience breakage, fines generation, or changes in appearance during conveying.
- Polymer industry: Polypropylene and polyethylene pellets, expanded polystyrene beads, engineering polymer granules, and specialty resin pellets may suffer chipping, dust generation, angel hair formation, abrasion, deformation, or contamination.
- Chemical industry: Porous catalyst particles, silica gel granules, molecular sieve beads, fertilizer granules, and specialty chemical crystals may degrade through impact, attrition, or abrasion.
- Petrochemical industry: Polyethylene and polypropylene resin pellets, polymer additives, catalyst powders, and certain porous catalyst carriers require careful handling to maintain particle integrity and minimize fines.
- Mineral industry: Lightweight expanded clay granules, porous mineral pellets, certain zeolite products, specialty ceramic granules, and friable mineral particles may fracture during transportation.
Selecting the Right Conveying Phase
One of the most important design decisions is selecting between dilute-phase and dense-phase conveying.
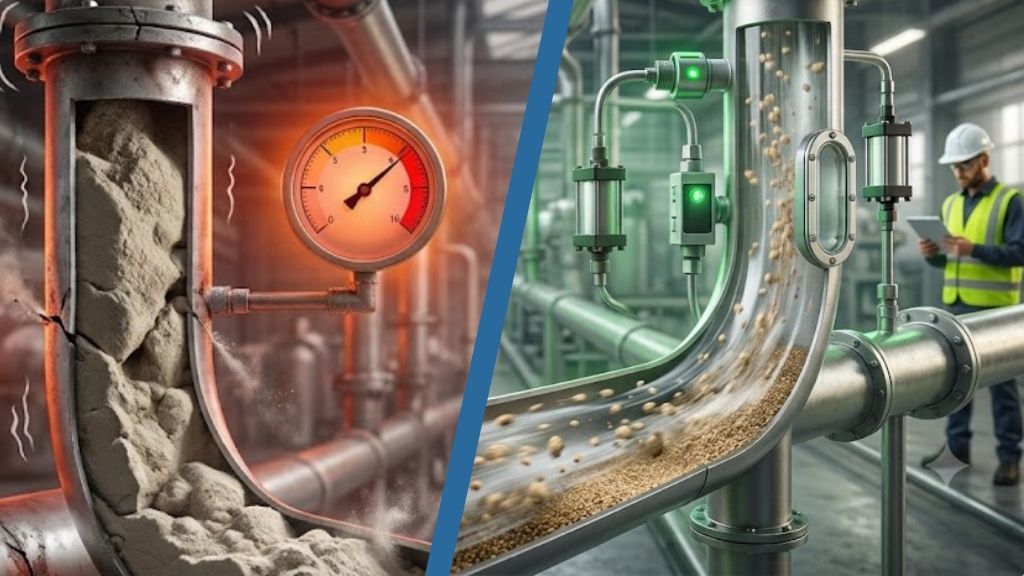
Dilute-phase conveying transports particles suspended in a relatively fast-moving air stream. It is widely used because of its flexibility, comparatively simple configuration, and suitability for many free-flowing materials. However, higher gas velocities can increase particle acceleration, collisions, and impact forces, potentially generating excessive fines.
Dense-phase conveying transports material at higher solids concentrations and often at lower gas velocities. Depending on the material and system configuration, it can reduce particle velocity and certain forms of impact damage. It is frequently considered for fragile polymer pellets, catalyst particles, and other products that benefit from gentler transport.
However, dense-phase conveying is not automatically the best solution. Poorly controlled plugs, excessive compression, unstable flow, and unsuitable pressure conditions can damage particles or cause blockages. Cohesive chemical powders and irregular mineral granules may also present challenges.
The objective is to identify the lowest practical conveying severity that maintains stable transport. This requires evaluating gas velocity, solids loading, pressure drop, feed consistency, pipeline geometry, and the material’s specific flow characteristics.
Pipeline Design: Reducing Impact and Attrition
Pipeline geometry has a direct influence on particle degradation. Straight sections, bends, reducers, diverters, and transitions can all affect particle trajectories and impact intensity.
Pipeline diameter is equally important. An undersized pipeline may require high velocities or generate excessive pressure losses, while an oversized pipeline may not maintain sufficient transport velocity under certain operating conditions.
Designers should evaluate the complete conveying route rather than focusing on a single nominal velocity. This includes local gas velocities, pressure changes, bend arrangements, feed points, and receiving equipment.
The goal is to minimize damaging interactions while preserving stable, uninterrupted material flow.
Feeder Selection and Controlled Material Acceleration
Particle damage can occur before material reaches the main conveying pipeline. At the feed point, solids accelerate from a relatively low velocity to the speed required for transportation. Poorly designed feeding arrangements can create sudden impacts, uneven material distribution, and excessive shear.
Feeder selection should consider more than throughput and pressure isolation. Engineers should evaluate particle entrapment, feed consistency, mechanical contact, acceleration severity, and the potential for degradation during startup and shutdown.
A well-designed conveying line cannot compensate for a feeder that damages the material before transportation begins.
Product Integrity as a Measurable Performance Target
A key principle in fragile-material conveying is that product protection must be defined through measurable acceptance criteria.
Specifications such as “minimum attrition” or “gentle handling” are difficult to verify unless the project defines acceptable product-quality changes.
Relevant measurements include:
- Percentage of fines generated below a specified particle size.
- Change in particle-size distribution between the inlet and outlet.
- Percentage of broken or chipped particles.
- Product recovery and material loss.
- Changes in bulk density, flowability, or functional properties.
- Contamination levels, where product purity is critical.
Balancing Energy Efficiency and Operating Cost
Energy consumption is an important consideration, but minimizing electricity use alone does not guarantee the most economical conveying system.
Lower gas velocities may reduce some forms of particle damage but can also increase the risk of deposition or blockage. Dense-phase systems may reduce gas consumption in suitable applications but require different pressure and control arrangements. A system designed without sufficient attention to product behavior may generate fines, increase waste, or experience costly downtime.
Consider a polymer facility where a lower-energy conveying system generates excessive pellet fines. The resulting material loss, cleaning requirements, and potential product-quality penalties may outweigh the energy savings. Similarly, excessive breakage of food products may reduce saleable yield, while catalyst degradation may increase downstream separation requirements.
A lifecycle cost assessment should therefore include capital expenditure, blower or compressor energy, maintenance, filter replacement, material losses, downtime, and the economic impact of degraded product.
The preferred design is the one that meets product-quality and safety requirements while delivering reliable operation at an acceptable total cost of ownership.
Automation, Monitoring, and Operational Reliability
Even a properly engineered system can damage fragile materials when operating conditions deviate from the intended range. Changes in feed rate, moisture, gas supply, filter condition, or receiving vessel pressure can affect conveying stability.
Monitoring should include relevant pressure readings, differential pressure, feed rate, gas flow, equipment status, and receiver levels. Abnormal pressure trends may indicate material buildup, restrictions, or unstable transport.
In a polymer plant, monitoring can help identify operating conditions associated with increased pellet damage. In chemical and mineral applications, pressure trends can help detect deposition or blockage before a complete interruption occurs. Food processing systems can use monitoring to support consistent throughput and reduce the risk of product loss.
Alarm thresholds and control logic should be established through engineering analysis and commissioning trials. Where justified, advanced analytics can identify deviations from normal operation and support early intervention.
The objective is to maintain the conveying system within a validated operating window, avoiding unstable flow and aggressive clearing cycles that may cause additional particle damage.
Conclusion
Designing pneumatic conveying systems for fragile materials requires a shift from capacity-driven engineering to material-focused design. Whether handling delicate food products, polymer pellets, porous chemical catalysts, petrochemical resins, or friable mineral granules, the fundamental objective remains the same: transport material while preserving its essential properties.
Success depends on understanding material fragility, selecting the appropriate conveying phase, optimizing pipeline geometry, controlling feeding and acceleration, defining measurable product-quality criteria, and validating performance through representative testing.
Equally important is the integration of energy efficiency, automation, safety, and lifecycle cost into the design process. No single parameter – whether velocity, pressure, pipeline diameter, or conveying phase—can independently guarantee gentle handling.
The true measure of a high-performance pneumatic conveying system is not simply how much material it transports, but how effectively it preserves product quality, minimizes waste, and delivers consistent performance throughout its operating life.